

The safeguard was never the country of finishing - it is the supplier documentation.
- 01
What changed
Commerce closed the transshipment route: rough shapes cut and formed in China but "finished" in Vietnam remain within scope of the antidumping order.
- 02
What it doesn't change
No fitting supplier - Baode included - can waive or reduce a duty rate that applies to your specific import.
- 03
What it does change
How costly a weak paper trail becomes the moment Commerce or CBP asks what you bought, and from whom.
Bottom line: ASME B16.9-compliant butt-weld elbows, tees, reducers and caps from Tianjin Baode Steel ship with heat-traceable mill test reports (MTR) and third-party inspection (TPI) as standard - not as an add-on.
2026 has been a tightening year for anyone importing steel pipe fittings into the United States. HTS heading 7307 has carried a 50% Section 232 duty since August 2025, and on August 28, 2026, the Federal Register published Commerce's amended covered-merchandise determination on the antidumping order for carbon steel butt-weld fittings from China - closing off a transshipment route through Vietnam that some importers had relied on. Neither development changes what a legitimate manufacturer should already be providing. It does change how much a weak paper trail can cost a buyer at customs.
This isn't customs or legal advice - duty classification depends on your specific HTS code, origin, and import structure, so a licensed customs broker should confirm your exposure. What we can speak to directly is the manufacturing and documentation side: what a compliant butt-weld fitting order should look like on paper, and where undocumented "cheap and fast" sourcing tends to fall apart.
Baode's Butt-Weld Fitting Program
One production line, four fitting families. Select a category to see scope, size range and applicable standards.

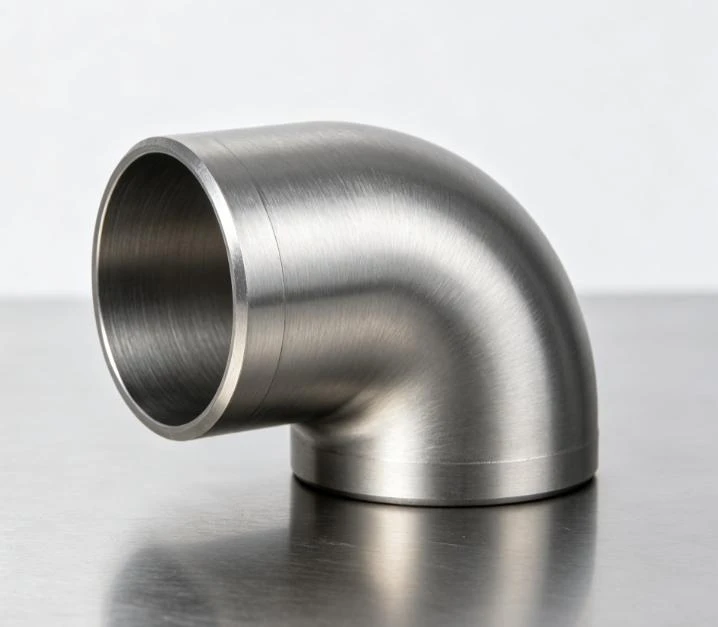
Butt-Weld Elbows
Engineered for permanent welded directional changes across a wide band of operating pressures and temperatures. 45°, 90° and 180° configurations, long radius (1.5D) and short radius (1.0D).
Seamless 1/2"–24"; welded up to 48". Material grades to ASTM A234, A403, A420 and A815, with beveled ends per ASME B16.25.
Tees & Lateral Tees
Equal (straight) and reducing tees for 90° branch connections, plus 45° lateral tees where a gradual flow transition is preferred over a hard turn.
Produced on dedicated tee-forming equipment from 1/2"–24" across a range of wall thicknesses. Carbon, stainless and alloy grades available - see the full tee program.
Concentric & Eccentric Reducers
Concentric reducers hold a common centreline; eccentric reducers keep one face flat - the standard choice at pump suction to prevent air accumulation and cavitation.
1/2"–48" in seamless, ERW, welded and fabricated construction. View reducer specifications →
Pipe Caps
Butt-weld caps for permanent line termination, formed to match the parent pipe schedule so wall thickness transitions stay smooth at the closure.
Produced on press lines alongside the reducer range, to ASME B16.9 dimensional requirements. Non-standard schedules handled as custom orders.
| Requirement | Standard / Range |
|---|---|
| Dimensions | ASME B16.9 |
| Carbon steel fittings | ASTM A234 WPB / WPC |
| Low-temperature fittings | ASTM A420 WPL6 |
| Stainless steel fittings | ASTM A403 (WP304/304L/316/316L/321/347) |
| Duplex / selected stainless | ASTM A815 |
| Seamless size range | 1/2" – 24" |
| Welded size range | up to 48" |
| End preparation | ASME B16.25 |
| Inspection & documentation | Project / purchaser specification |
Carbon Steel, Stainless Steel, or Alloy
Grade selection follows the line, not the catalogue. Select a material family to see the typical service envelope and the grades we hold.
Carbon Steel - ASTM A234 WPB
Oil & gas gathering, power generation, water treatment. The default grade for general industrial pressure piping.
Stainless Steel - ASTM A403 WP316L
Chemical processing, food-grade lines, corrosive environments needing molybdenum-added resistance.
Alloy Steel - WP11 / WP22 / WP91
High-temperature, high-pressure service. Project specs should be submitted before quoting to confirm heat treatment parameters.

Documented Direct-Mill vs. Unverified Transshipment
The August 2026 ruling was about one specific evasion pattern - rough shapes cut in China, "finished" in Vietnam, and entered as Vietnamese-origin. But the underlying lesson applies to sourcing decisions generally: a supplier who can't produce heat-traceable paperwork is a supplier who can't tell you what you're actually importing.
| Factor | Documented Direct-Mill Supply | Unverified / Undocumented Supply |
|---|---|---|
| Heat number traceability | ✓ Full MTR issued per heat/lot | ✕ Often missing or generic |
| Dimensional standard | ✓ ASME B16.9 checked and stated | ✕ Assumed, rarely verified in writing |
| Third-party inspection (TPI) | ✓ Coordinated on request, pre-shipment | ✕ Not offered, or re-negotiated each time |
| Origin documentation | ✓ Consistent, matches production records | ✕ Prone to mismatched third-party paperwork |
| NDE & mechanical testing | ✓ PMI / UT / MT / PT / hydrostatic, on scope | ✕ Test results unavailable or undated |
| Import risk if audited | ✓ Records available to support your filing | ✕ Buyer left without evidence to respond |
Note: no fitting supplier - Baode included - can waive or reduce a duty rate that applies to your specific import. What documentation changes is your ability to demonstrate exactly what you bought and from whom, should Commerce or CBP ask.
Quality Control on Every Order
Dimensional inspection runs alongside material verification on every production lot: OD, wall thickness, center-to-end, centerline radius, angle, end squareness and ovality - then chemical composition, tensile strength, yield strength, elongation, and impact testing on low-temperature grades.
Non-destructive examination options include PMI, ultrasonic testing (UT), magnetic particle testing (MT), dye penetrant testing (PT) and hydrostatic testing, coordinated with TPI schedules per the applicable certification scope. Every shipment traces back to a heat number.
5 Steps to Verify a Compliant Supplier
A repeatable checklist you can hand to any supplier before the PO is confirmed.
Request the mill test report (MTR) with a specific heat number for the exact lot being shipped - not a template.
Confirm the dimensional standard (ASME B16.9) is stated on the drawing or spec sheet, not just implied verbally.
Match the material grade (A234 / A403 / A420 / A815) to your project spec before production, not after.
Agree the TPI scope - dimensional check, NDE method, and hydrostatic test if required - before the PO is confirmed.
Verify export paperwork - certificate of origin, packing list, commercial invoice - is consistent with production and MTR records before the container ships.
Why Buyers Work With Tianjin Baode Steel

Tianjin Baode Steel Co., Ltd operates a dedicated pipe-fitting factory in Yanshan County, Cangzhou, producing carbon, stainless and alloy steel elbows, tees, reducers, caps and flanges alongside seamless and welded steel pipe.
Certifications include ISO 9001, ISO 14001, ISO 45001 and AAA Credit Enterprise status. Fittings ship to more than 40 countries and regions across North America, South America, Southeast Asia, the Middle East and Africa.
FAQ
Click a question to expand the answer.
It depends on your specific HTS classification, entry history, and whether an existing AD/CVD order applies to your goods. The August 2026 determination addressed rough-shape fittings finished in Vietnam; it did not create new duties on standard direct-from-China shipments. Confirm applicability with a licensed customs broker - this is general manufacturing information, not customs advice.
Material test reports are issued as standard practice, traceable to heat number. Third-party inspection is coordinated according to your purchase order - scope and inspecting body should be agreed before production begins.
Standard configurations ship within 15 days outside of peak season, extending to around 30 days during peak demand periods. MOQ starts at 1 piece; larger project orders should confirm scheduling in advance.
Yes. Non-standard centerline radii, heavy or intermediate wall schedules, and specialized alloy grades are handled as custom engineering orders. Submit the project specification before quoting so forming, heat treatment and testing parameters can be evaluated.
Material test certificates, dimensional inspection records, and third-party inspection reports (where scoped) are supplied in line with the agreed procurement terms, alongside standard commercial and export documents.
Need MTR-backed, ASME B16.9-compliant butt-weld fittings?
Send the angle, radius, size, schedule, material grade and testing scope - we'll come back with a quote and a documentation package you can hand to your broker.
Request a Quote →Disclaimer: Technical data is for reference only. Please confirm critical specifications before purchase. This article is general manufacturing and sourcing information, not customs, legal, or trade-compliance advice - consult a licensed customs broker for duty and origin determinations specific to your shipment. Tianjin Baode Steel Co., Ltd assumes no liability for misuse or misapplication of products.


